In the field of thread cutting tools, most rotary tools are only responsible for cutting in a single direction of rotation (such as drills, milling cutters, reamers, and gear hobs). The cutting behavior generated by other thread trajectories is mostly generated by the rigid motion trajectory of mechanical equipment. The above-mentioned tools face the risk of tip breakage if they reverse. UGMIC believes that "reciprocating thread cutting tools such as taps and dies" are very unique tools. Their function belongs to the special cases of all tool categories. In addition to rotating and cutting threads, taps and dies also need to use synchronous feed pitch equipment to meet the cutting shape of the thread path. In the narrow hole thread machining space, they must complete the removal of thread material, preserve the threaded part, cut cooling, cut lubrication, avoid high temperature annealing of the tool, high temperature fusion and adhesion of the workpiece, poor chip removal and chip adhesion, and damage to the thread surface. They also need to meet the requirements of chip breaking, chip removal, complete preservation of the thread, and maintaining the precision of each threaded workpiece product when the thread cutting tool reaches the bottom of the tap and then reverses to withdraw.
UGMIC believes that the function of thread cutting tools and taps is not just to form the thread profile, but to handle the following simultaneously :
forward cutting (feed-in program) → thread formation (feed-in program) → reverse retraction (retraction program) → chip removal (full program) → friction reduction (full program) → cutting load control (full program) → maintaining thread
quality (full program).
Therefore, the tool structure directly affects the machining results.
4.1 Taps groove
The main tap chip removal groove structure may include:
• Straight groove type (no forced chip removal)
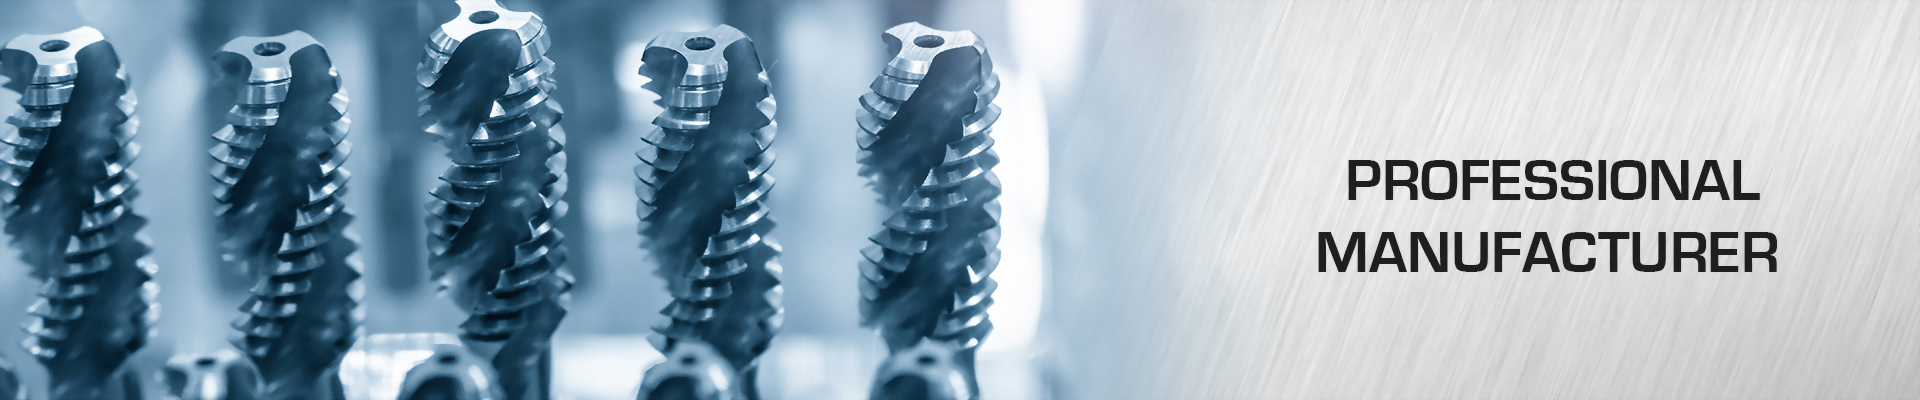
• Spiral groove type (forced rear chip removal)
• Pointed groove type (forced front chip removal)
• Roll Form type (no chips, no chip removal issues, but has a springback problem)
• Interrupted thread structure (optimizes chip removal path and increases chip removal space)
• Straight groove + Interrupted thread composite structure (optimized chip removal path, increased chip removal space)
• Spiral groove + Interrupted thread composite structure (forced rear chip removal + optimized chip removal path, increased chip removal space)
• Special cutting edge (forced front chip removal + 2P guide teeth meet the requirement of not penetrating the bottom of the threaded hole)
• Special thread profiles (V-shaped thread, trapezoidal thread, winged thread, circular thread)
• Central cooling (central water outlet internal cooling port)
• Special chip removal structure
• Special shank and size design (dedicated machine side fixed shank, milling cutter shank)
• Custom tooling structures (double-layer taps with the same pitch, double-layer taps with different pitches, tap plates with different pitches)
Different structures are not simply product classifications, but rather correspond to different processing problems.
Forample :
Straight Tap (StT) are generally suitable for :
⚫ Threaded chips: Suitable for powder, flakes, and granular chips.
⚫ Threaded hole types: Blind hole & Through hole
⚫ Usage: Mechanical or manual
⚫ Material application parameter notation: #O, #CH, #C, #BC, #A, #AS
Pointed Tap (PoT) is generally suitable for :
⚫ Threaded chips: Suitable for flake chips and long chips.
⚫ Threaded hole type: can only penetrate through the hole.
⚫ Usage: For mechanical use
⚫ Material application parameter notation: #O, #C, #A
Spiral Taps (SpT) are generally suitable for :
⚫ Threaded chips: Suitable for flake chips and long chips.
⚫ Threaded hole types: Blind hole & Through hole
⚫ Usage: For mechanical use
⚫ Material application parameter notation: #O, #CH, #C, #A,
Related to chip removal direction, blind hole machining, and chip removal.
Roll Form Tap (RFT) is generally suitable for
⚫ Thread cutting: Chipless, extruded thread
⚫ Threaded lower hole diameter: Based on thread specification accuracy
⚫ Threaded hole types: Blind hole & Through hole
⚫ Usage: For mechanical use
The effects of eliminating chip interference on workpiece thread quality, friction control, and reduced compressive load are achieved.
Interrupted structure tap (X)
This is a very important direction for chip removal structure optimization in UGMIC's reciprocating thread cutting tool technology.
Core objective :
• Reduce the number of teeth involved in cutting simultaneously
• Reduce thread friction
• Improve the chip removal path and space of the thread.
• Reduce thread chip adhesion
• Improve thread surface
• Reduce threading torque
• Improve the threading stability of viscoelastic materials
Straight Tap + Interrupted structure (StT-#X)
This mainly results in a combined effect of chip removal capability, friction control, and cutting load dispersion.
Straight Tap + Interrupted structure+ Central cooling (StT-#X-H)
This mainly results in a combination of the following effects: chip removal capacity × friction control × cutting load reduction × enhanced chip removal × forced cooling × forced lubrication × reduced chip interference with workpiece thread quality.
Pointed Tap + Interrupted structure (PoT-#X)
This mainly results in a combined effect of chip removal capability, friction control, cutting load dispersion.
Spiral Tap + Interrupted structure (StT-#X)
This mainly results in a combined effect of chip removal capability, friction control, and cutting load dispersion.
Spiral Tap + Interrupted structure + Central cooling (StT-#X-H)
This mainly results in a combination of the following effects: chip removal capacity × friction control × cutting load reduction × enhanced chip removal × forced cooling × forced lubrication × reduced chip interference with workpiece thread quality.
Roll Form Tap + Central Cooling Structure (RFT-H)
This mainly results in a combination of effects: friction control, reduced compressive load, forced cooling, forced lubrication, and elimination of chips that interfere with the quality of the workpiece thread.
4.2 Threading tool-tap parameters
Tool parameters can be categorized as follows :
Threading tool geometry parameters
• Tap thread size
• Tap thread pitch
• Tap thread profile
• Tap thread angle
• Threading tool tap groove
• Number of threads cut by tap
• Tap thread interrupted structure
• Thread rake angle of tap
• Thread back angle of tap
• Thread relief angle of tap
• Cutting edge shape of threading tools
Threading tool dimensions
• Tap shank diameter (JIS, DIN, Side-Fix Shank, Mill-Shank )
• Tap overall length (JIS, DIN, UGMIC stock)
• Tap Thread cutter effective length
• Tap Thread cutter work Length
• Tap Thread Lead start
• Tap Thread accuracy ( Based primarily on the accuracy of the dental gauge.)
• Tap thread oversize tool size (Primarily based on increasing the dimensions according to the precision of dental gauges)
Threading tool functional parameters
• Tap surface treatment (Coating)
• Tap central cooling (Inner cooling)
• Tap special chip removal (Interrupted)
• Tap special wear-resistant design (Relief angle)
• Tap customized structure
Tap parameter markings match workpiece material
With over 35 years of accumulated practical experience, UGMIC has continuously developed its unique thread cutting tool parameter marking technology. Each fixed-size thread cutting tool has a matching parameter mark for the most suitable thread workpiece material. For different workpiece material application parameters, each type of reciprocating thread cutting tool from UGMIC must correspond to a unique workpiece material matching parameter mark. This unique workpiece material parameter mark is the result of practical application and optimization verification, enabling users to obtain the most ideal thread cutting tool usage experience and value.
Straight Flute Taps Solid /Welded Carbide (StT.SC/StT.WC)
|
Flute Type |
Tool |
Material of Workpiece |
Chamfer |
Hole type |
Chip Type |
Thread size |
|
|
|
|
||||||||
|
|
||||||||
|
|
||||||||
|
Straight |
#A |
Hard Steel, Hardness>40HRC, Plastic+fiber, Cast Iron, Bakelite, No lead Bronze, Zine |
Ⅰ Ⅱ Ⅲ |
Throught/ Blind |
Powdery/ short |
4≦D≦160 0.8≦P≦3.0 |
||
|
Straight |
#B |
Bronze, NO lead Brass |
Ⅲ |
Throught/ Blind |
Powdery/ short |
8≦D≦160 0.8≦P≦3.0 |
||
|
Straight |
#BC |
Brass |
Ⅲ |
Throught/ Blind |
Powdery/ short |
8≦D≦160 0.8≦P≦3.0 |
||
|
Straight |
#C |
Soft steel/ Iron, Titanium Alloy ,Tool Steel, Stainless Steel |
Ⅱ |
Throught |
longer chip |
8≦D≦160 |
||
|
Aluminum Alloy(6061-T6,ADC) |
Ⅱ/Ⅲ |
Throught/ Blind |
Powdery/ short |
8≦D≦160 |
||||
|
Straight |
#CHRP |
Copper Pipe |
Ⅱ |
Throught |
longer chip |
8≦D≦160 |
||
|
Aluminum(AC),Iron |
Ⅱ/Ⅲ |
Throught/ Blind |
Powdery/ short |
8≦D≦160 |
||||
|
Straight |
#O |
Aluminum Alloy(6061-T6,ADC) , Aluminum(AC), Copper Pipe |
Ⅱ |
Throught |
longer chip |
3≦D≦6 |
||
|
Cast Iron, Bakelite, No lead Bronze, Bronze, NO lead Brass, Brass |
Ⅱ/Ⅲ |
Throught/ Blind |
Powdery/ short |
3≦D≦6 |
||||
|
Straight |
#OC |
Tool Steel, Stainless Steel, Titanium Alloy |
Ⅱ |
Throught |
longer chip |
3≦D≦6 |
Spiral Flute Taps Solid /Welded Carbide (SpT.SC/SpT.WC)
Flute Type
Tool
Material of Workpiece
Chamfer
Hole type
Chip Type
Thread size
Spiral
#A
Hard Steel,
Hardness>40HRC,
Plastic+fiber, Cast Iron,Bakelite, No lead Bronze, Zine
Ⅲ
Throught/ Blind
longer /short
5≦D≦60
Spiral
#C
Brass, Aluminum Alloy(6061-T6,ADC) ,Soft steel/ Iron,
Titanium Alloy
Ⅲ
Throught/ Blind
longer /short
5≦D≦60
Spiral
#CHRP
Aluminum(AC)Copper Pipe
Ⅲ
Throught/ Blind
longer /short
8≦D≦60
Spiral
#O
Aluminum Alloy(6061-T6,ADC) , Aluminum(AC), Copper Pipe
Ⅲ
Throught/ Blind
longer /short
3≦D≦6
Spiral
#OC
Tool Steel, Stainless
Steel, Titanium Alloy
Ⅲ
Throught/ Blind
longer /short
3≦D≦6
Mark
Length
0.8≦P≦2.0
0.8≦P≦2.0
1.0≦P≦2.0
0.5≦P≦1.0
0.5≦P≦0.7
Fluteless (Roll) Taps Solid Carbide (RFT.SC)
|
Flute Type |
Tool |
Material of Workpiece |
Chamfer |
Hole type |
Chip Type |
Thread size |
|
Fluteless |
4P |
Aluminum Alloy(6061-T6,ADC) , Aluminum(AC)Copper Pipe Soft steel/ Iron, Titanium Alloy, Tool Steel, Stainless Steel, Titanium Alloy |
Ⅱ |
Throught |
longer |
1.6≦D≦20 |
|
Fluteless |
2P |
Aluminum Alloy(6061-T6,ADC) , Aluminum(AC)Copper Pipe Soft steel/ Iron, Titanium Alloy, Tool Steel, Stainless Steel, Titanium Alloy |
Ⅲ |
Blind |
longer |
1.6≦D≦20 |
Spiral Flute Taps HSS-CO (SpT.Hc)
|
Flute Type |
Tool |
Material of Workpiece |
Chamfer |
Hole type |
Chip Type |
Thread size |
|
Spiral |
#C |
Aluminum Alloy(6061-T6,ADC) , Aluminum(AC)Copper Pipe Soft steel/ Iron, Titanium Alloy, Tool Steel, Stainless Steel, Titanium Alloy |
Ⅲ |
Throught/ Blind |
longer |
8≦D≦60 |
UGMIC summarizes common options for thread cutting tools:
1. Tap shape = JIS shank × DIN shank × Milling cutter shank × Side fastening shank
2. Tap groove = Straight groove (StT) × Tip groove (PoT) × Spiral groove (SpT) × Extrusion groove (RFT)
3. Tap material = Cobalt-containing high-speed steel (Hc) HSS-Co × Solid carbide (SC) × Welded carbide (WC)
4. Main workpiece material parameter notation: (#O) × (#CH) × (#C) × (#BC) × (#B) × (#A) × (#AS)
5. Additional parameter notation (#R) × (#P) (Optional)
6. Center water outlet structure (H) - Optional
7. Thread skipped tooth structure (#X)- Optional
The above options summarize the common materials and structural elements of tapping tools:
1.Tap shape × 2.Tap groove × 3.Tap material × 4.Thread specification & accuracy ×5.Workpiece material parameter mark (#C) × 6.Additional chip removal option × 7.Optional = forced cooling, lubrication, chip removal)
UGMIC offers precision taps with various options including tap shape, tap flutes, tap material, and parameter markings, as follows :
For example :
⚫ Spiral tap - cobalt-containing high-speed steel
JIS shank. Spiral tap. (HSS-Co)High-speed steel with cobalt content M12*1.5-6H-#C = (J.SpT.Hc-M12-*1.5-6H-#C)
#C will be transformed into #O, #CH, #B, #A, etc., depending on the material properties of the applicable workpiece.
⚫ Spiral tap - (HSS-Co) - center cooling - Interrupted thread structure
JIS shank-Spiral tap-(HSS-Co) M12*1.5-6H-#CX-H = (J.SpT.Hc-M12-*1.5-6H-#CX-H)
#C will be transformed into #O, #CH, #B, #A, etc., depending on the material properties of the applicable workpiece.
⚫ Roll Form Taps-HSS-Co
JIS Shank-Roll Form Taps-HSS-Co- M12*1.5-2P-RH10 = (J.SpT.Hc-M12-*1.5-2P-RH10)
⚫ Straight Taps- Solid
Carbide
JIS shank-Straight tap-Solid carbide M10*1.5-6H-#A = (J.StT.SC-M10*1.5-6H-#A)
#A will be transformed into #O, #CH, #C, #B, etc., depending on the material properties of the applicable workpiece.
⚫ Straight Taps- (Brazed) Welded Carbide
JIS shank-Straight tap-Welding Carbide M20*1.5-6H-#A = (J.StT.WC-M20*1.5-6H-#A)
#A will be transformed into #O, #CH, #C, #B, etc., depending on the material properties of the applicable workpiece.
⚫ Pointed Taps- Solid Carbide
JIS Shank -Pointed Taps- Solid Carbide M10*1.5-6H-#C = (J.PoT.SC-M10*1.5-6H-#C)
#C will be transformed into #O, #CH, #B, #A, etc., depending on the material properties of the applicable workpiece.
⚫Spiral Taps- Solid Carbide
JIS Shank- Spiral Taps- Solid Carbide M10*1.5-6H-#C = (J.SpT.SC-M10*1.5-6H-#C)
#C will be transformed into #O, #CH, #B, #A, etc., depending on the material properties of the applicable workpiece.
⚫ Spiral Taps-Welding Carbide
JIS Shank - Spiral Taps-Welding Carbide M20*1.5-6H-#C = (J.SpT.WC-M20*1.5-6H-#C)
#C will be transformed into #O, #CH, #B, #A, etc., depending on the material properties of the applicable workpiece.
⚫ Roll Form Tap-Solid Carbide
JIS Shank- Roll Form Tap-Solid Carbide M12*1.5-2P-RH10 = (J.SpT.SC-M12-*1.5-2P-RH10)
⚫ Roll Form Tap-Solid Carbide-Center cooling
JIS Shank - Roll Form Tap-Solid Carbide-Center cooling M12*1.5-2P-H-RH10 = (J.SpT.SC -M12-*1.5-2P -RH10-H)
⚫Straight Taps- Solid Carbide–Interrupted-Center Cooling
JIS Shank-Straight Taps- Solid Carbide-Interrupted -Center Cooling M10*1.5-6H-#CX-H = (J.StT.SC-M10*1.5-6H-#CX-H)
#C will be transformed into #O, #CH, #B, #A, etc., depending on the material properties of the applicable workpiece.
⚫ Straight Tap- Welded Carbide – Center Cooling- Interrupted
JIS Shank- Straight Tap- Welded Carbide– Center Cooling- Interrupted M20*1.5-6H-#CX-H = (J.StT.SC-M20*1.5-6H-#CX-H)
#C will be transformed into #O, #CH, #B, #A, etc., depending on the material properties of the applicable workpiece.
⚫ Spiral Taps-Solid Carbide-Center cooling-Interrupted
JIS Shank- Spiral Taps-Solid Carbide-Center cooling-Interrupted M10*1.5-6H-#CX-H = (J.SpT.SC-M10*1.5-6H-#CX-H)
#C will be transformed into #O, #CH, #B, #A, etc., depending on the material properties of the applicable workpiece.
⚫ Spiral Taps-Welded Carbide-Center cooling-Interrupted
JIS Shank- Spiral Taps-Welded Carbide-Center cooling-Interrupted M20*1.5-6H-#CX-H = (J.SpT.WC-M20*1.5-6H-#CX-H)
#C will be transformed into #O, #CH, #B, #A, etc., depending on the material properties of the applicable workpiece.
UGMIC has accumulated over 35 years of experience in manufacturing thread cutting tools and providing solutions to thread problems. It categorizes thread cutting tool materials, groove types, and application parameters for at least 250 material models (excluding thread specifications and precision standards) to address potential issues related to various workpiece material physical properties, thread specification precision requirements, machining conditions, etc., and recommends relevant optimization solutions.
Author: Dr. Chen, Wenliang
Ph.D. in Mechanical & Aeronautical Engineering
Thread Tool Development & Manufacturing Specialist
UGMIC Industrial Ltd.
Last updated: August 12, 2026